Industry operating context

Where cold chain operations lose performance—and what evidence helps decide.

Industrial performance and reliability context for cold rooms, chilled or frozen handling, process interfaces, logistics support, and refrigeration-dependent operations.

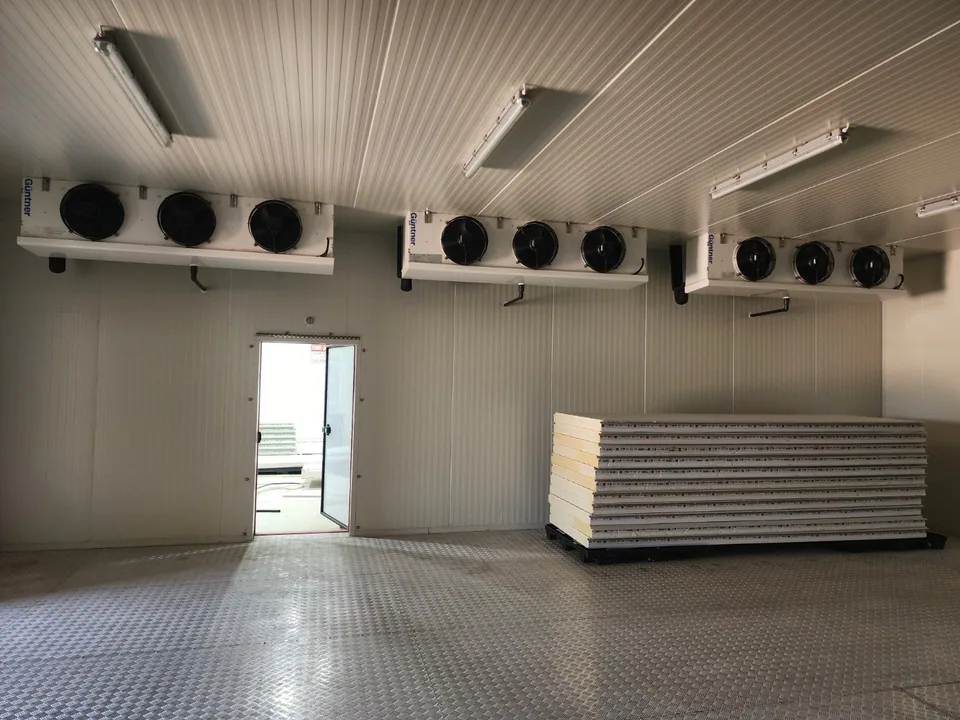
Three ceiling-mounted cold-room evaporator units inside an insulated cold space.
Machinery, utilities & process interfaces

Assets and interfaces that shape the operating context.

  • Cold rooms, blast or process chilling interfaces, doors, seals, fans, and evaporator areas
  • Conveyors, pumps, packaging, loading, and handling systems around chilled or frozen product
  • Temperature records, alarms, defrost routines, and operating-state evidence
  • Electrical supply, standby power, controls, and monitoring interfaces within agreed scope
  • Refrigeration plant interfaces only where competent specialist involvement is defined
Common operating problems

Patterns that deserve structured investigation.

  • Temperature instability, product holds, or unclear loss of cold-chain control
  • Repeated fan, door, seal, conveyor, pump, or handling-equipment defects
  • Defrost, loading, door-opening, cleaning, or operating practices affecting performance
  • Incomplete maintenance, alarm-response, inspection, or verification records
  • Unclear boundary between machinery condition, refrigeration performance, and operating practice
Operational, safety & continuity exposure

Consequence should be understood before the intervention is chosen.

  • Product loss or quality hold from unverified temperature control
  • Production or dispatch interruption from equipment or utility failures
  • Electrical, controls, refrigerant, pressure, food-safety, or statutory decisions outside direct scope
  • False confidence when temperature records, alarms, or corrective actions are incomplete
Buyer decision questions

Clarify the decision before selecting the engineering response.

These questions do not diagnose the factory from a webpage. They help management identify what must be understood next.

01

Is the main consequence product temperature, production continuity, dispatch delay, energy use, equipment condition, or unverified records?

02

What evidence separates operating practice, door or airflow condition, controls, electrical supply, machinery condition, and specialist refrigeration performance?

03

Which next step is justified: preserve records, inspect, measure, repair, monitor, improve operating practice, or escalate to a competent specialist?

Controlled public problem areas

Start from the operating problem—not from a product or discipline.

Only problem families already approved for public use are shown here. A problem can cross multiple disciplines, so the first task is to frame the decision and evidence correctly.

Equipment Reliability

Equipment keeps failing, tripping, wearing out, or returning to the same defect.

Problems where machinery condition, repeated failure, criticality, maintenance quality, or asset history may be driving operational loss.

Discuss this problem
Production Performance

Production is below target, unstable, bottlenecked, or losing too much time.

Problems where throughput, utilisation, recurring stops, constraints, operating practice, or equipment interaction may be limiting output.

Discuss this problem
Maintenance System

Maintenance is reactive, poorly recorded, difficult to plan, or not closing repeat defects.

Problems involving preventive maintenance, work control, asset registers, spare parts, responsibilities, failure history, and maintenance evidence.

Discuss this problem
Measurement and Operational Data

A decision depends on information the factory does not reliably measure or record.

Problems where runtime, cycles, energy, temperature, pressure, vibration, production state, downtime, or another operational signal is missing or unreliable.

Discuss this problem
Operational Evidence

Work is being done, but records, ownership, verification, or close-out evidence are weak.

Problems involving controlled records, inspection evidence, action ownership, handover, maintenance traceability, and proof that agreed work was completed and verified.

Discuss this problem
Cause Not Yet Clear

Something is wrong, but the factory does not yet know whether the cause is mechanical, operational, utility, control, data, or process related.

A neutral entry route for problems that should be classified through evidence rather than requiring the client to diagnose the issue before contacting an engineer.

Discuss this problem
Related decision guides

Relevant problem guides for this sector.

These links connect sector context to controlled public diagnostic questions. They do not assume that the same root cause applies across factories.

Browse the complete Problem Library
A disciplined first-pass lens

Move from operating context to the next defensible decision.

01

Define the cold-chain decision, measurement boundary, product/process context, and required evidence before recommending changes

02

Separate door, airflow, loading, defrost, equipment, electrical, control, and specialist refrigeration factors

03

Use operating records, temperature evidence, maintenance history, and observations to decide the next safe route

04

Escalate refrigeration design, refrigerant, pressure, electrical, controls, food-safety, and statutory matters to competent resources where required

Measurement, workflow & technology readiness

Technology should answer an operating question—not lead the diagnosis.

Industrial Sensing

Temperature, door-state, airflow, pressure, current, and alarm evidence may support defined operating decisions when the measurement boundary is clear.

Industrial Data Acquisition

Existing controllers, loggers, or manual records may support trend and verification work where data quality, access, and responsibility are confirmed.

Maintenance Systems

Inspections, alarm response, defrost checks, door/seal work, action closure, and verification records can be structured before any controlled system pilot.

Review the technology and delivery boundary
Start with the industrial problem

Discuss an operating problem in your cold chain operations.

Share the affected process or machine, operating consequence, evidence already available, location, and the decision you need to make. Scope and competence boundaries are confirmed before work begins.